Recommended High-Performance Packaging Lines
Engineered for global quick-service restaurants, retail meal deliveries, catering enterprises, and multi-unit chains. Explore our precision-manufactured takeaway food containers.
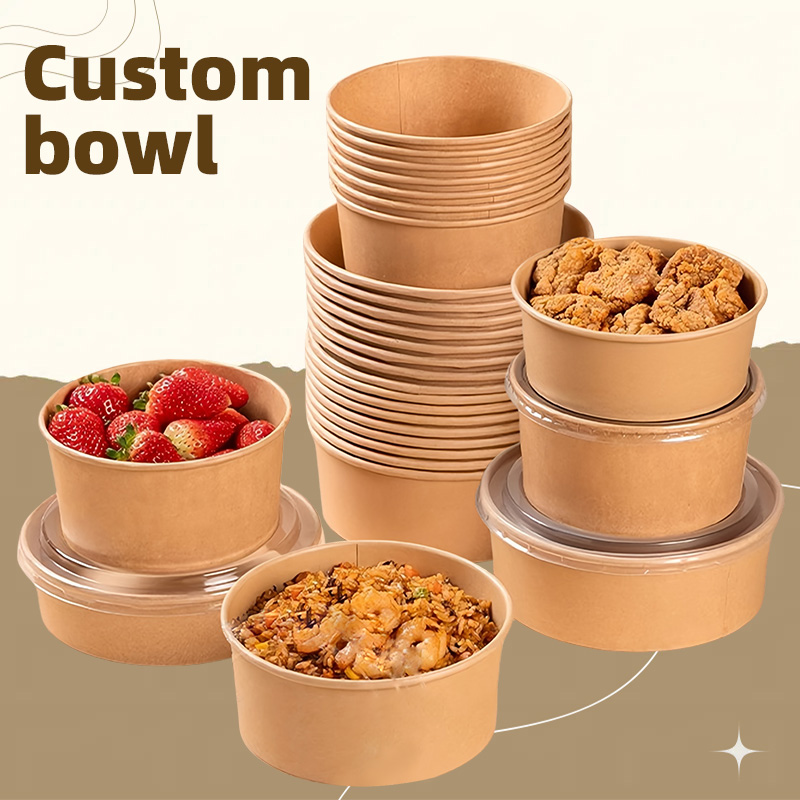
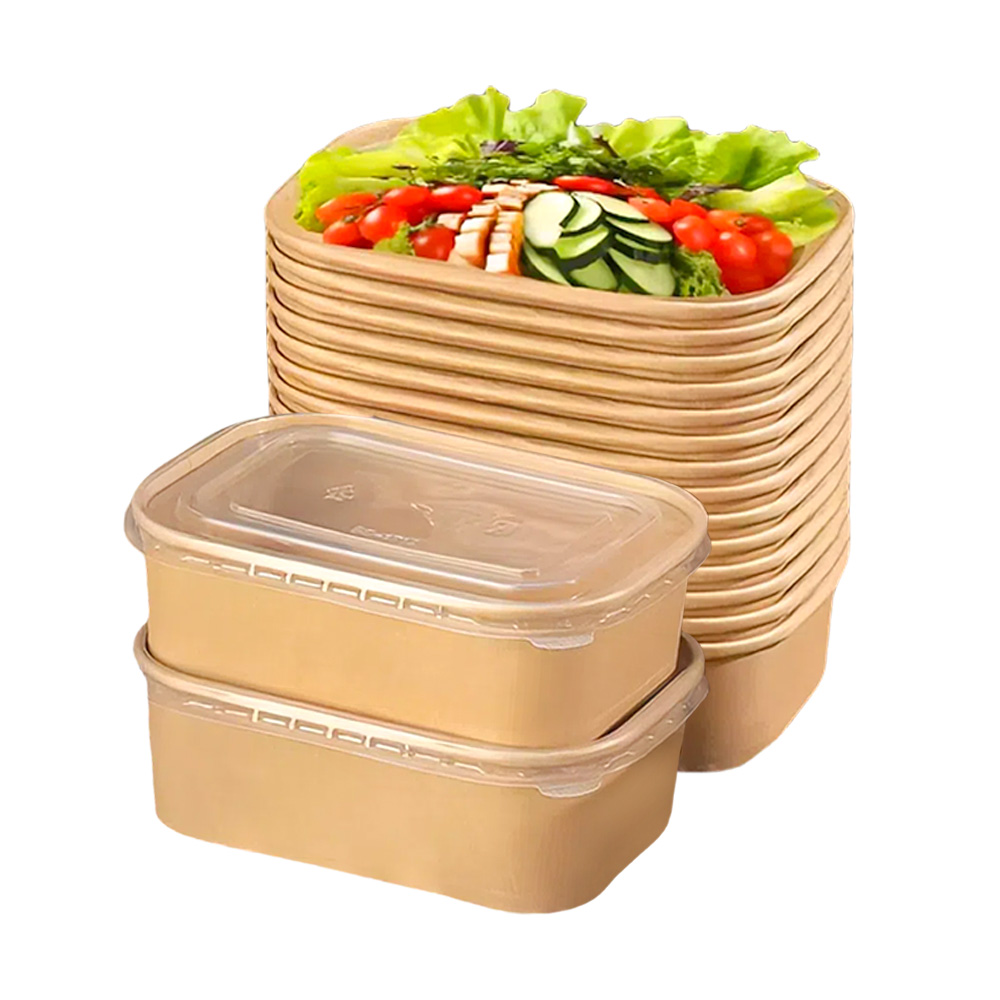
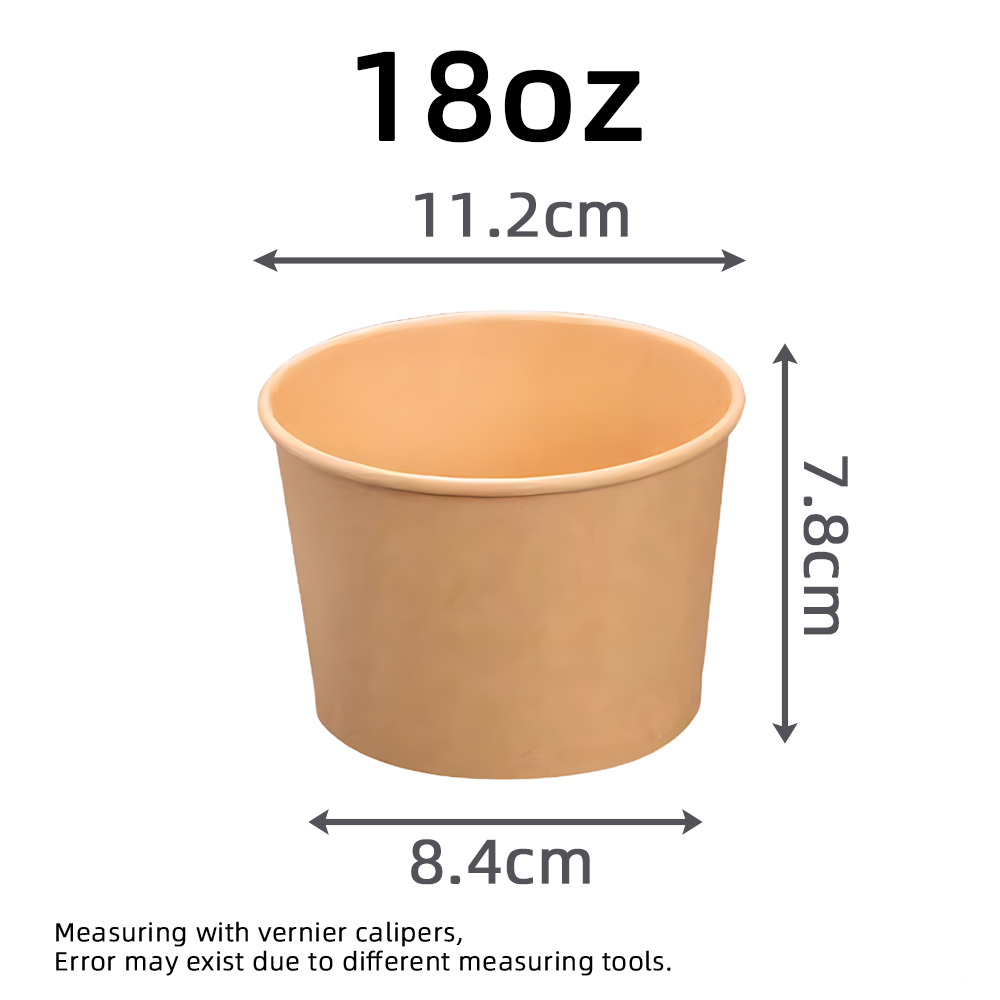
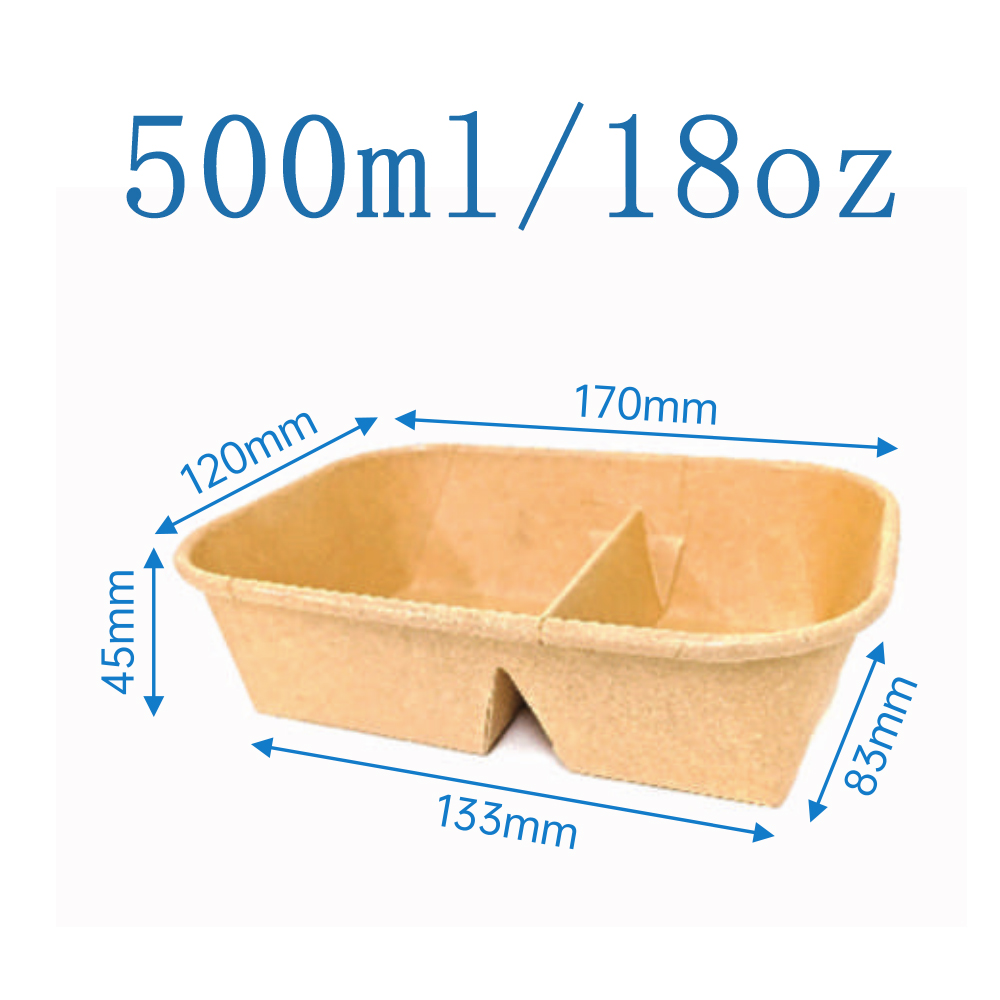
Industrial White Paper: Global Takeaway Packaging Engineering
Comprehensive manufacturing standards, food-contact compliance (FDA / BfR / EU No 10/2011), and high-barrier structural dynamics for commercial buyers.
As the international food logistics sector pivots toward stringent ecological mandates and tamper-evident packaging integrity, commercial takeout lunch boxes have evolved from simple folding paperboard into sophisticated barrier-engineered systems. Global brand aggregators, cloud kitchen operators, and institutional hospitality purchasers now mandate strict adherence to multi-tier criteria: mechanical stacking resilience under humid thermal conditions, oil and grease resistance (OGR) without per- and polyfluoroalkyl substances (PFAS-free), and absolute organoleptic neutrality so zero paperboard odors migrate into delicate culinary dishes.
1. Substrate Chemistry and Polymeric Barrier Deposition
The manufacturing architecture of industrial-grade food boxes begins at raw fiber selection. Premium takeaway packaging utilizes virgin unbleached kraft paperboard manufactured from long-fiber coniferous wood pulp, typically ranging between 280 gsm and 350 gsm in basis weight. The mechanical matrix delivers superior burst strength and ring-crush resistance, essential for multi-layer stacking inside delivery carrier bags. To resist liquids ranging from boiling broths to dressing-heavy vinaigrettes, substrates receive inline functional coatings:
| Coating / Barrier Matrix | Thermal Boundary Limits | Oil & Grease Resistance (Kit Test) | Regulatory Status & Disposal Route |
|---|---|---|---|
| Traditional Polyethylene (PE) | -18°C to +95°C (Freezer to Warm) | Kit 12 (Superior, Non-penetrating) | FDA 176.170 / EU compliant; Standard mechanical repulping |
| Polylactic Acid (PLA Bio-liner) | -10°C to +85°C (Chilled to Hot) | Kit 9 - 11 (High Performance) | ASTM D6400 / EN 13432; Industrial composting infrastructure |
| Aqueous Dispersion Coating (Water-based) | -20°C to +120°C (Microwaveable) | Kit 7 - 10 (Controlled Resistance) | Zero Fluorochemicals; Directly curbside repulpable & recyclable |
| Polypropylene (PP Extruded) | -20°C to +125°C (Full Microwave Safe) | Kit 12 (Immune to lipid degradation) | High steam barrier; Highly stable for fatty and boiling stews |
At our Luohe manufacturing plant, continuous spectrophotometric and Cobb-testing protocols monitor water absorption rates, ensuring the inner coated boundary keeps the outer cellulose dry, rigid, and thermally insulating during 45-minute transport cycles.
2. Structural Integrity and Leak-Proof Rim Tooling
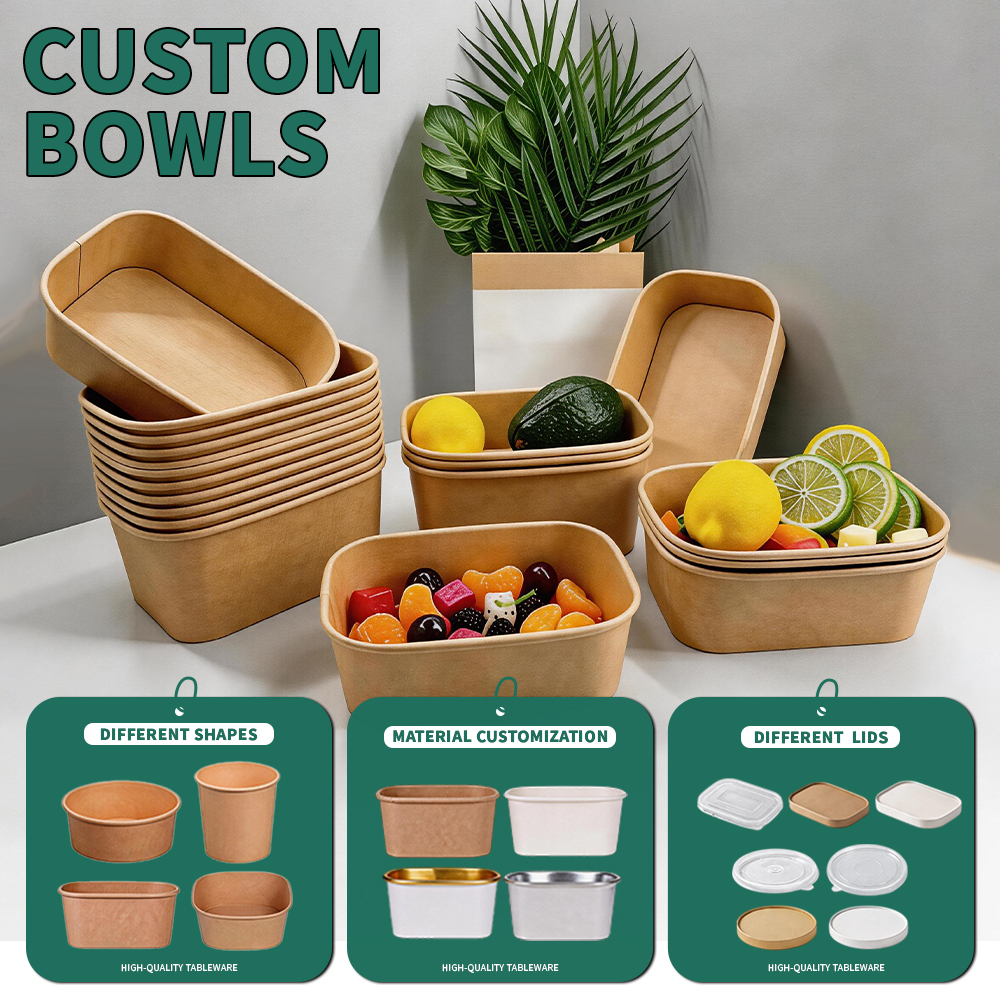
A frequent failure point across standard disposable containers is rim deformation under axial load, causing lid detachment and liquid spillage. Our high-precision forming machinery employs automated multi-station curling stations that produce dense, double-rolled perimeter rims. This geometric configuration maximizes hoop strength, enabling airtight snap fits with thermoformed lids (PET, PP, or molded pulp) that stay sealed during transport. For rectangular folding lunch boxes, our machines leverage laser-cut dies, precision-creased folding scores, and ultrasonic or thermoseal bonding to eliminate adhesive breakdown caused by steam.
Macro Trends Shaping Takeaway Packaging Procurement
Actionable market intelligence for procurement directors navigating circular economy policies, supply chain resilience, and global import regulations through 2026-2030.
PFAS Elimination Mandates
Regulatory authorities across the US, EU, and UK have instituted zero-tolerance thresholds on added fluorochemicals historically used for oil-proofing.
- Adoption of bio-based aqueous barriers and physical calendering.
- Mandatory third-party total organic fluorine (TOF) testing documentation.
- Full compliance with BfR Recommendation XXXVI and FDA guidelines.
Circular Repulpability
Enterprise buyers are moving beyond single-stream industrial composting claims to universally recyclable, fiber-reclaimable paper substrates.
- Water-dispersible barrier formulations that dissolve during re-pulping.
- Decreased carbon footprint along maritime shipping corridors.
- Alignment with European Packaging and Packaging Waste Regulation (PPWR).
Compartmentalized Engineering
Food delivery aggregator applications have triggered a surge in demand for segmented multi-dish containers that eliminate flavor cross-contamination.
- Precision-molded division walls engineered for structural stacking.
- Differential venting: crisp food sections stay aerated, gravies remain sealed.
- 15-20% space optimization compared to individual multi-tub systems.
Branding & Anti-Counterfeiting
Packaging now acts as the primary customer-facing billboard for ghost kitchens and premium franchise networks.
- Food-contact soy-based inks using high-speed 6-color flexographic printing.
- Matte, tactile, and natural unbleached kraft aesthetic accents.
- Integrated dynamic QR code imprinting for loyalty verification and tracking.
Enterprise Advantages: Luohe Temip Plastic Products Co., Ltd.
SGS-verified direct manufacturing capabilities, Henan food corridor logistics, and end-to-end quality validation protocols.
Headquartered in the Dongcheng Industrial Agglomeration Zone, Zhaoling District, Luohe City, Henan Province, Luohe Temip Plastic Products Co., Ltd. benefits directly from operating inside one of China's most advanced food-processing hubs. Proximity to major food-ingredient processors, dairy combines, and automated industrial packagers provides our engineering teams with immediate insights into practical operational demands. Packaging design is not simulated in isolation; our containers undergo continuous validation against real grease matrices, varied temperature stresses, and mechanical delivery vibrations.
SGS On-Site Verified
Independent third-party audits verify cleanroom conditions, automated line capacities, and documented QA/QC procedures across all production phases.
Raw Material Source Inspection
Incoming paperboard reels and virgin resin pellets undergo spectrographic, thickness, and tensile checks before introduction to production floor lines.
Fortune 500 Qualified
Demonstrated fulfillment pedigree executing multi-million unit annualized procurement programs for international hospitality and supermarket brands.
Flexible OEM/ODM Engineering
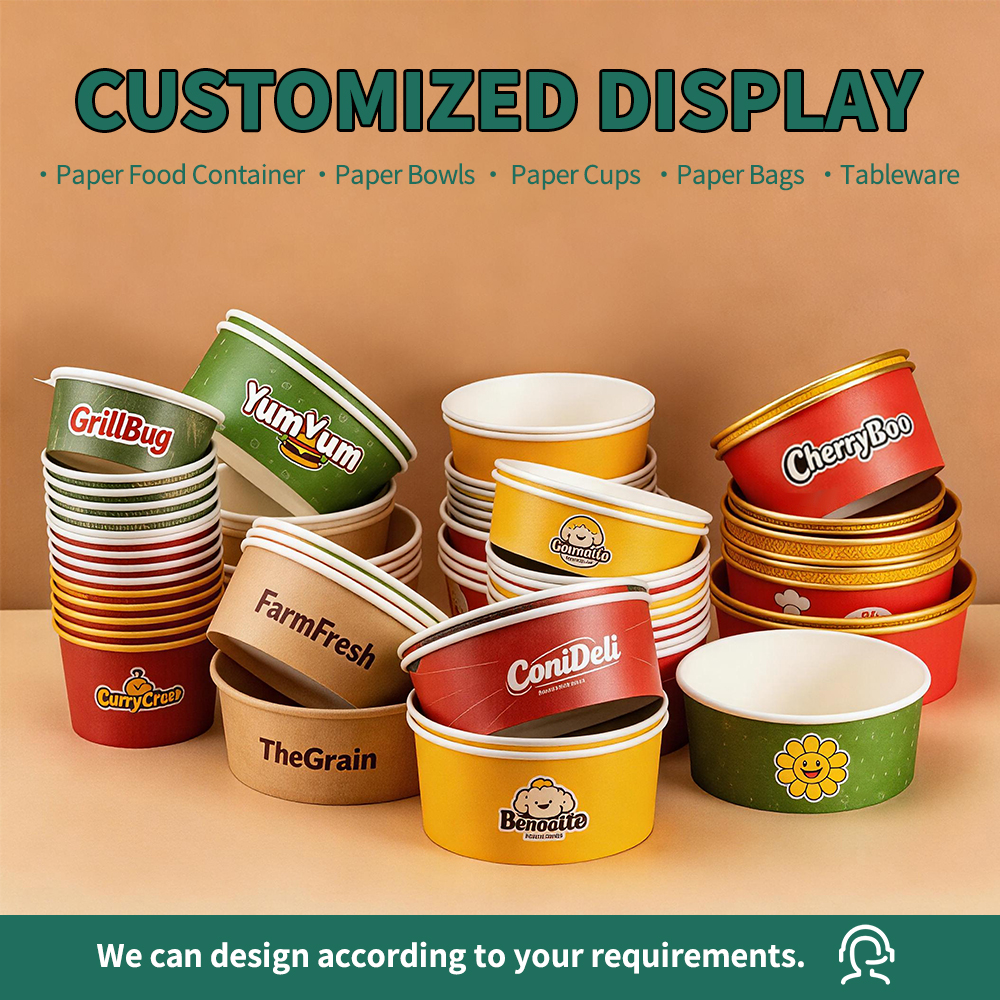
From minor artwork branding adjustments to ground-up customized structural molding, our CAD tooling teams provide rapid prototyping in under 5 business days.
Our 2,200m² factory space employs 37 skilled technicians, operating high-speed cup formers, automated bowl crimpers, high-precision roll-fed die cutters, and inline optical defect scanners. Verified buyer feedback consistently records a 4.3/5 TrustPass score, cementing our reputation as a trusted manufacturing partner across North America, Europe, Oceania, and the GCC.
International Procurement & Technical FAQ
Direct technical answers addressing regulatory oversight, minimum run sizes, container compatibility, and global export shipping logistics.
Q: How do your lunch boxes verify compliance with FDA and EU food-contact frameworks?
Our raw materials are sourced strictly from accredited pulp and paper mills maintaining current FSC, FDA 21 CFR 176.170, and EU No 10/2011 compliance records. We routinely submit finished product lots to SGS and Intertek for overall migration, heavy metal extraction, and sensory evaluations.
Q: What are the standard Minimum Order Quantities (MOQ) for custom brand printing?
For standard off-the-shelf formats without branding, MOQs start as low as 10,000 to 20,000 units. For custom flexographic or offset-printed branding using our automated color management systems, initial runs typically begin at 30,000 to 50,000 units per SKU, depending on dimensions.
Q: Can paper takeaway containers safely withstand microwave reheating and oil exposure?
Containers coated with high-barrier aqueous dispersion or specialized Polypropylene (PP) linings are fully microwaveable up to 120°C for standard meal reheating cycles without peeling or chemical leaching. For high-oil dishes, our formulations achieve a Kit 12 rating, blocking oil seepage completely.
Q: What lid pairing choices are provided for round and rectangular lunch boxes?
We supply a comprehensive suite of matching lid formats: crystal-clear anti-fog PET lids for cold foods, high-heat micro-vented PP lids for hot gravies, unbleached matching kraft paper pressed lids for cohesive branding, and molded bagasse pulp lids for plastic-free packaging programs.
Q: How do you prevent packaging damage and moisture absorption during sea freight?
All finished cartons are packed into heavy-duty 5-ply corrugated export master cases, lined with moisture-barrier polyethylene master bags, and vacuum-sealed where required. Palletized loads are machine stretch-wrapped with corner-board protectors, preventing compression collapse inside marine shipping containers.
Q: What is the lead time from design sign-off to port loading in China?
Digital design proofing and structural dieline mockups are generated within 48 hours. Physical pre-production samples are completed in 3 to 5 business days. Once production samples receive client sign-off, full container-load (FCL) volume orders ship within 15 to 22 business days directly from Qingdao or Shanghai ports.
Ready to Upgrade Your Global Foodservice Packaging Supply?
Connect with our senior technical engineering and export sales department to request certified testing documentation, material samples, and tailored factory-direct quotations.