Precision-Engineered Food Containers & Hinged Clamshell Cartons
Manufactured under strict ISO9001 and food-contact compliance. Explore our standard and custom-molded high-barrier takeout vessels ready for volume export.
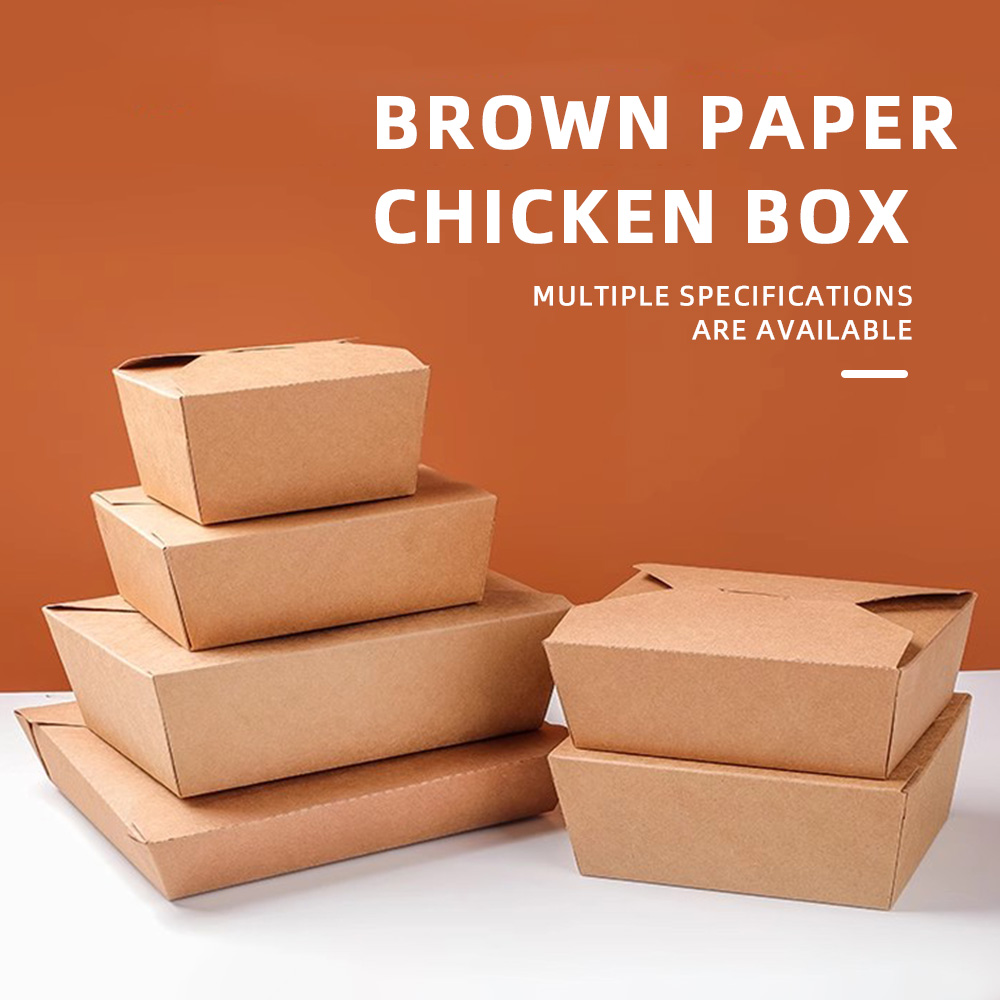
Custom Logo Kraft Paper Food Boxes Foldable Takeout Packaging
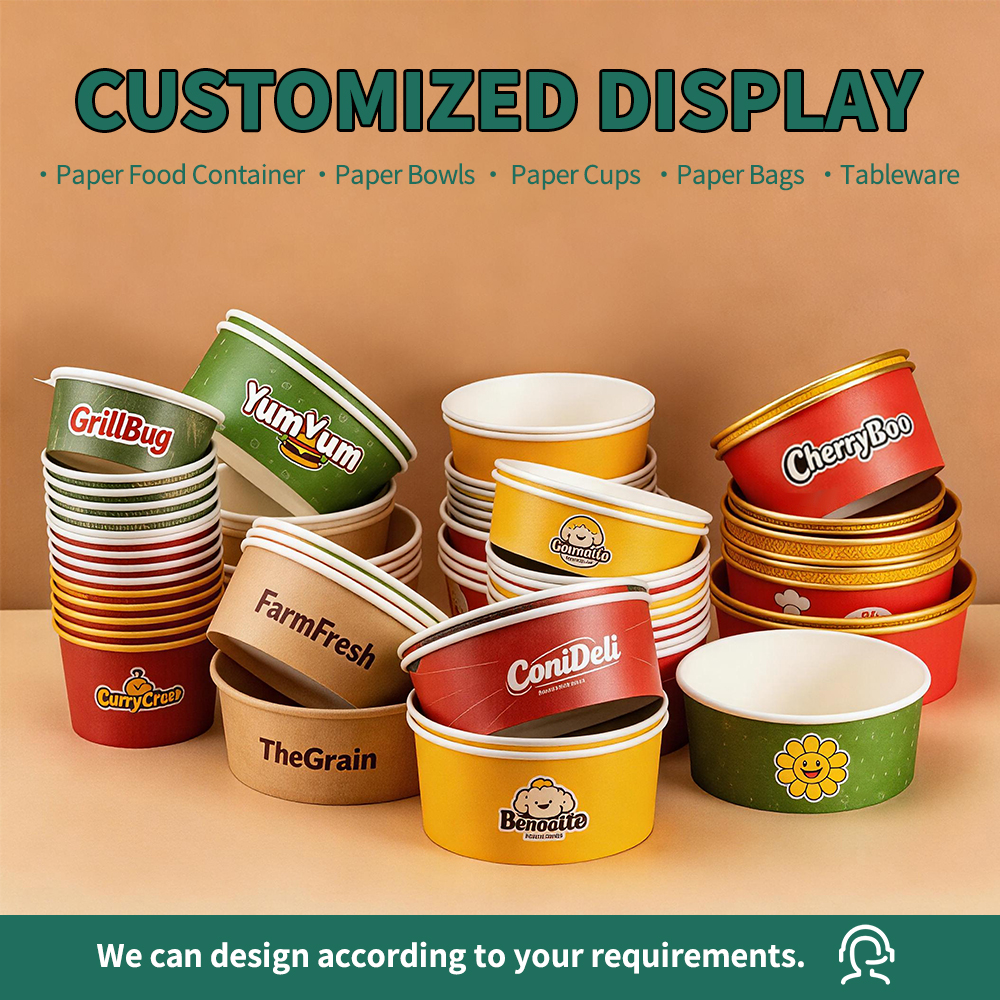
Custom Logo Kraft Paper Salad Bowls 500-1450ml With Lids
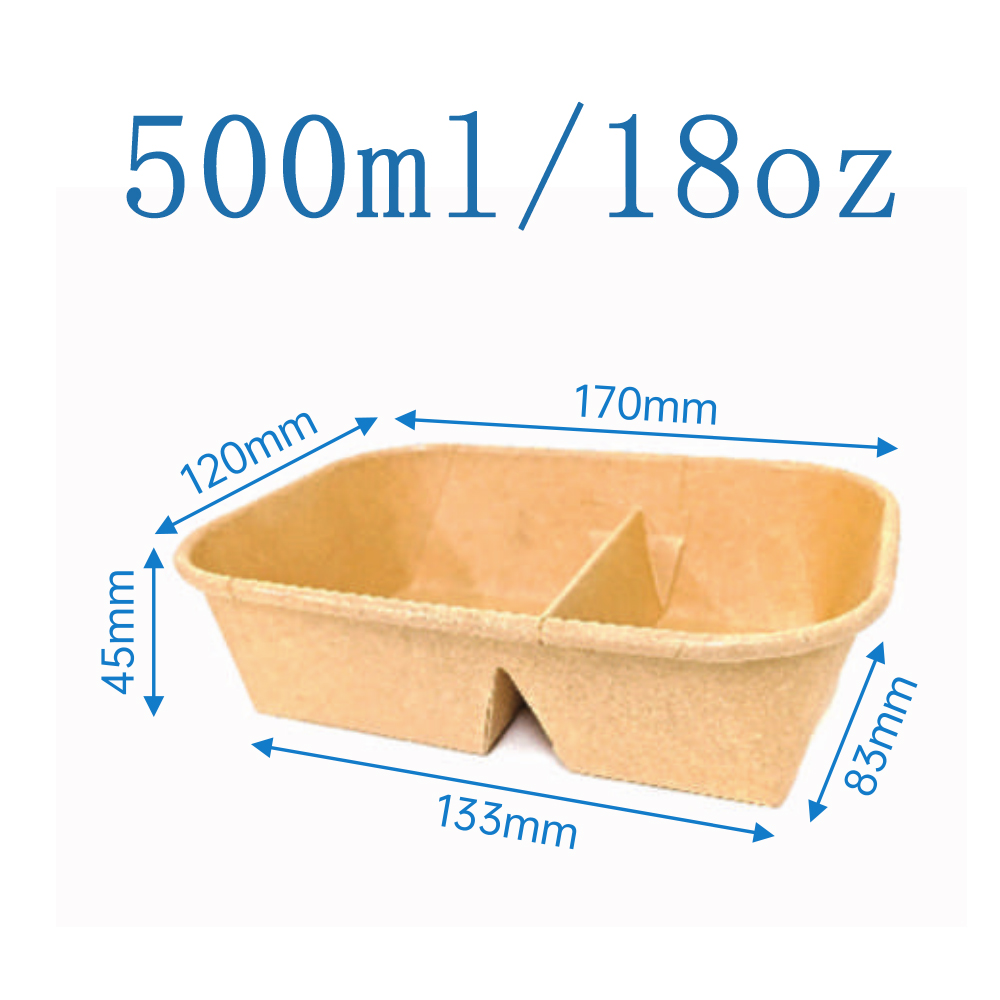
Rectangle 2 Divisions 500ml 18oz Disposable Kraft Food Cartons
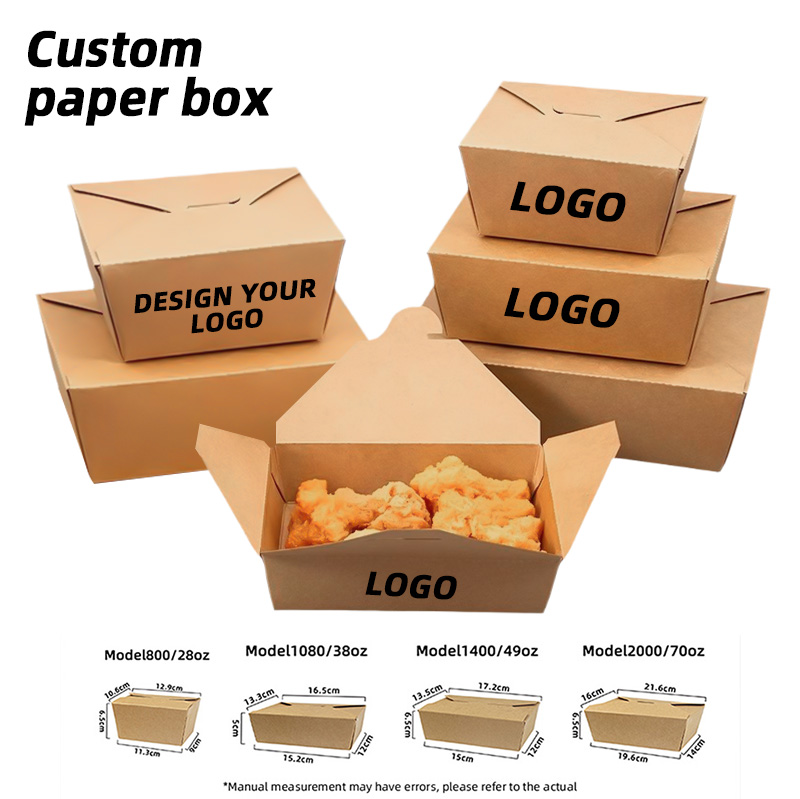
Recyclable Kraft Paper Food Boxes Oil-Proof Foldable Containers
Disposable Kraft Paper Containers Square Bowls With Fitted Lids
Factory Supply 18oz/500ml Kraft Rectangular Salad Paper Bowls
Biodegradable Disposable Kraft Paper Food Cartons & Takeaway Plates
Biodegradable Kraft Paper Bowls 500-1450ml Microwave Safe With Lids
Engineering Excellence in Hinged Food Packaging: China Manufacturing Baseline
In high-throughput commercial foodservice, the structural integrity of hinged food containers determines consumer brand perception, kitchen packing efficiency, and last-mile delivery success. As one of China's premier specialized packaging manufacturing facilities based in the Dongcheng Industrial Agglomeration Zone of Luohe, Henan—the heartland of the nation's high-standard food processing supply chain—our engineering protocols address the physical stressors that off-the-shelf packaging fails to withstand.
A true high-performance hinged food container must achieve an exact equilibrium: it requires sufficient caliper thickness (typically 300gsm to 380gsm virgin unbleached kraft or solid bleached sulfate) to prevent thermo-mechanical wall buckle under stacking loads, paired with high-precision die-cut scoring along the hinge axis. Substandard hinges fatigue and tear after repeated opening and closing cycles or crack when exposed to steaming contents exceeding 85°C. Our automated forming lines deploy multi-stage pneumatic creasing matrices that compress fiber bundles without fracturing the cellulose outer layer, guaranteeing over 200 flex cycles at full operational resilience.
SGS Audited Facility Compliance: Every production lot leaving our 2,200m² manufacturing facility adheres to strict raw-material batch verification, water-contact Cobb60 absorption tests under 12g/m², and TAPPI T 559 Kit oil-repellency ratings exceeding Level 9 without utilizing banned per- and polyfluoroalkyl substances (PFAS).
Why Tier-1 Importers & Global Restaurant Chains Partner With Us
From initial rapid-tooling CAD prototyping to automated high-volume die-cutting, we mitigate systemic supply chain risk for global procurement directors.
SGS-Verified Manufacturing
Full on-site audit clearance covering structural consistency, cleanroom environmental controls, and traceable raw material origin documentation.
- Zero-PFAS certification verified
- Complete BRCGS / FDA / LFGB dossiers
Precision Tooling & OEM/ODM
Full-custom tooling for custom embossed lids, vented closures, asymmetric internal compartment dividers, and ergonomic front thumb-tab releases.
- CAD/CAM rapid sampling within 5 days
- Proprietary vent geometry options
Industrial Food Cluster Scale
Strategically situated in Henan's massive food production cluster, slashing inbound pulp and polymer raw-material freight times and input volatility.
- High-speed flexographic 6-color printing
- Daily container shipping via Qingdao port
Fortune 500 Qualified Audit
Long-term contract manufacturer for leading multinational restaurant groups requiring rigorous supply continuity and multi-point QA checks.
- Optical automatic defect scanning
- Batch-traceable barcode integration
Comparative Performance Engineering: Substrate Matrix
Evaluating barrier coatings, thermal ceilings, grease repellency, and regulatory recyclability for overseas retail and commercial kitchen integration.
| Substrate Formulation | Coating / Barrier Type | Thermal Window | Kit Grease Value | Compostability / Recyclability | Recommended Food Group |
|---|---|---|---|---|---|
| Aqueous Dispersion Kraft | Water-Based Polymer Dispersion | -20°C to +115°C | Kit Level 10-12 | Standard Paper Mill Recyclable (PTS) | Gravy Meals, Asian Curries, Fried Chicken |
| Industrial Bio-Kraft | Extruded PLA (Polylactic Acid) | -15°C to +85°C | Kit Level 9-11 | EN 13432 Industrial Composting | Cold Greens, Poke Bowls, Gourmet Wraps |
| High-Yield Virgin Board | PE (Polyethylene) Extrusion | -30°C to +100°C | Kit Level 12+ | Specialized Poly-Recovery Only | Ultra-Hot Broths, High-Steam Noodles |
| Mineral-Filled PP (MFPP) | Natural Calcium Carbonate (40%) | -10°C to +125°C | Impervious (Barrier) | RIC #5 Polypropylene Streams | Heavy Roast Carvery, Oily Barbecue |
| Molded Sugarcane Bagasse | Fluorine-Free Internal Sizing | -25°C to +120°C | Kit Level 7-9 | Home & Industrial Compostable | Quick-Serve Burgers, Bakery, Dry Snacks |
Navigating Global Regulatory Shifts: EU PPWR, SUPD, and US State PFAS Prohibitions
For international supply chain managers, packaging compliance is no longer a tertiary checklist item—it is an existential operational threshold. The rollout of the European Union's Packaging and Packaging Waste Regulation (PPWR), alongside stringent national implementations of the Single-Use Plastics Directive (SUPD), is rapidly disqualifying conventional plastic-lined and fluorochemical-treated food packaging.
Simultaneously in North America, legislation across California (AB 1200), New York, and Washington has outright banned detectable organic fluorine in food service ware. In response, our engineering laboratory in Henan pioneered ultra-refined aqueous dispersion coatings. Unlike legacy coatings that melt into unrecoverable microplastic slurries during pulping, our water-based dispersion dissolves cleanly within standard hydropulpers, achieving a repulpability yield exceeding 98.4%. This allows European and American importers to classify containers as standard recyclable paper waste, shielding downstream distributors from prohibitive EPR (Extended Producer Responsibility) packaging eco-taxes.
Future Procurement & Product Trends in Hinged Containers (2025–2030)
Emerging structural modifications, material evolutions, and smart-packaging transitions reshaping global B2B foodservice tenders.
Dynamic Vapor-Release Micro-Venting
Condensation is the single greatest cause of fried food sogginess during 30-minute delivery transit. Next-generation hinged containers integrate micro-embossed moisture louvers that selectively release steam while trapping sensible heat and preventing liquid slosh.
- Preserves battered crust crunch index
- Zero particulate entry from road transit
Tool-Integrated Tamper Evidence
Eliminating adhesive safety stickers saves kitchen labor and removes adhesive contaminants from paper recycling loops. Sourcing trends favor clamshells featuring structural break-away tear strips molded directly into the hinged perimeter lock.
- Clear visual food security confirmation
- Eliminates extra label consumables cost
Ultra-Compact Nesting Compression
With international shipping and warehousing expenses fluctuating wildly, nested stacking profile optimization is critical. Our modern tooling reduces sleeve nested height by 24%, increasing shipping container carton density up to 1,200 cartons per 40ft HQ.
- Lowest landed cost per packaged unit
- Seamless automatic dispenser de-nesting
Frequently Asked Questions for Importers & Procurement Teams
Addressing essential technical parameters, tooling lead times, MOQ flexibility, and containerization logistics.
What is the standard production MOQ for custom logo flexo printing?
For stock tool designs requiring customized branding (up to 6 colors flexographic or offset), our baseline minimum order quantity is 30,000 to 50,000 units per SKU depending on container volume. For completely custom physical molds and dimensions, production runs begin at 100,000 units with full tooling amortization schedules available.
How do your paper hinged containers perform against boiling liquids and oil seep?
Our containers are precision-engineered using high-density virgin wood pulp paired with aqueous barrier coatings that resist hydrostatic pressure from boiling sauces and hot soups up to 100°C without pinhole delamination. All stock lines achieve oil penetration resistance beyond TAPPI Kit Level 10 for continuous durations exceeding 4 hours.
Can you provide comprehensive third-party food contact test reports?
Yes. As an SGS-verified production facility, every export formulation carries recent, fully traceable migration test certifications for FDA 21 CFR 176.170, EU Regulation 1935/2004, LFGB, and rigorous total fluorine screenings confirming absolute zero PFAS additions.
How are samples produced and shipped for quality validation?
We provide unprinted plain samples from existing production stock free of charge within 48 hours for immediate physical fill-and-seal testing. Custom-dimension 3D samples or digitally printed prototypes are completed within 5 to 7 business days and dispatched via express air freight (DHL/FedEx) directly to your testing lab.
What is the typical lead time from final artwork sign-off to port loading?
Standard repeated orders typically clear production in 15 to 22 business days. First-time bespoke tool-molded orders run between 28 and 35 days to allow for die CNC cutting, pilot sample approval, and cleanroom validation. Our plant offers consolidated container loading to optimize multi-SKU ocean freight.
Can your containers handle microwave heating and blast-chill freezers?
Our aqueous-coated and unbleached kraft substrates are certified microwave-safe up to 120°C for up to 3 minutes without structural collapse or chemical off-gassing. For frozen meal distribution, our board fibers retain tensile toughness down to -25°C without brittle cracking along the score lines.
Partner Directly With China's Leading Packaging Engineering Factory
Secure stable factory-direct pricing, guaranteed capacity allocation, and fully certified sustainable hinged food packaging for your regional distribution network.